Integrated Cycling Solutions & Factory Product Lines
In addition to our precision OEM CO2 inflators, our TÜV Rheinland-assessed manufacturing floor produces turnkey bicycle equipment, mobility platforms, cargo systems, and workshop accessories for international brands.
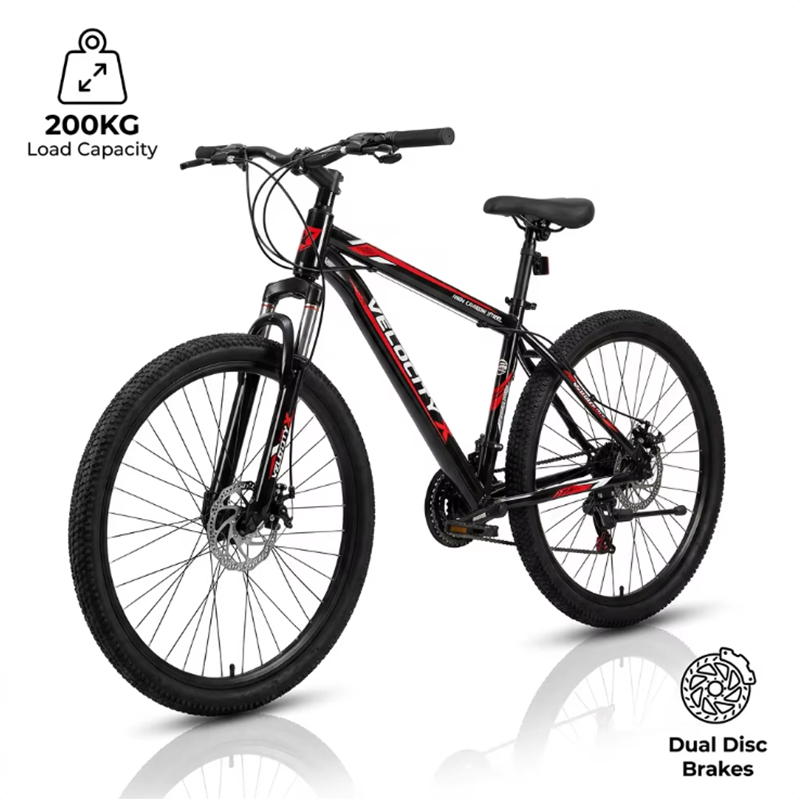
ESLNF 24-Inch Speed Dual-Disc Brakes High-Carbon Steel Frame Bicicletas MTB
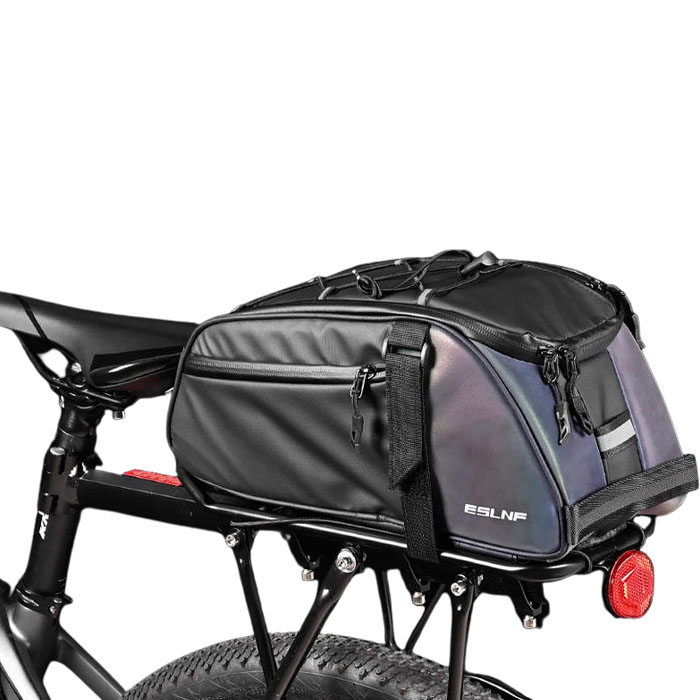
ESLNF Waterproof Large Capacity Reflective Cycling Cargo Trunk Carrier Bag
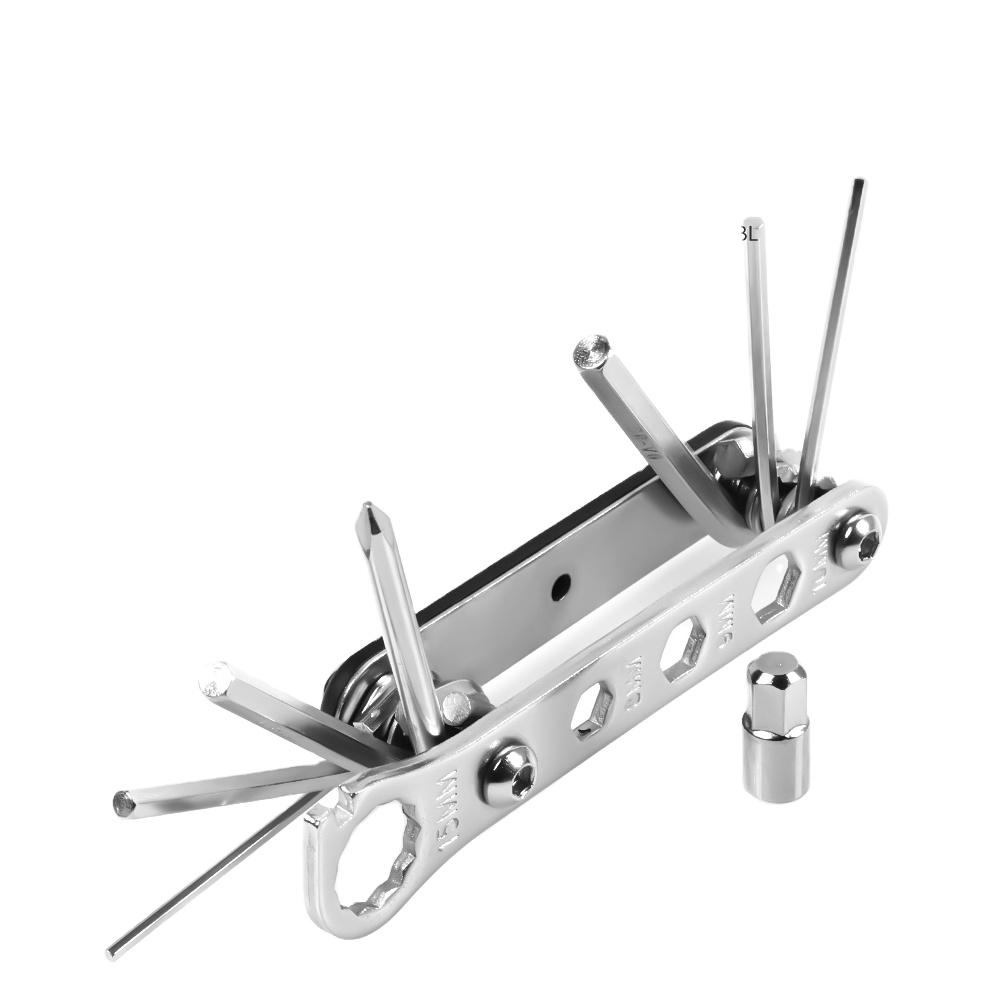
13 In 1 Portable Folding Combination Mini Tool Multifunctional Bicycle Tool Kit
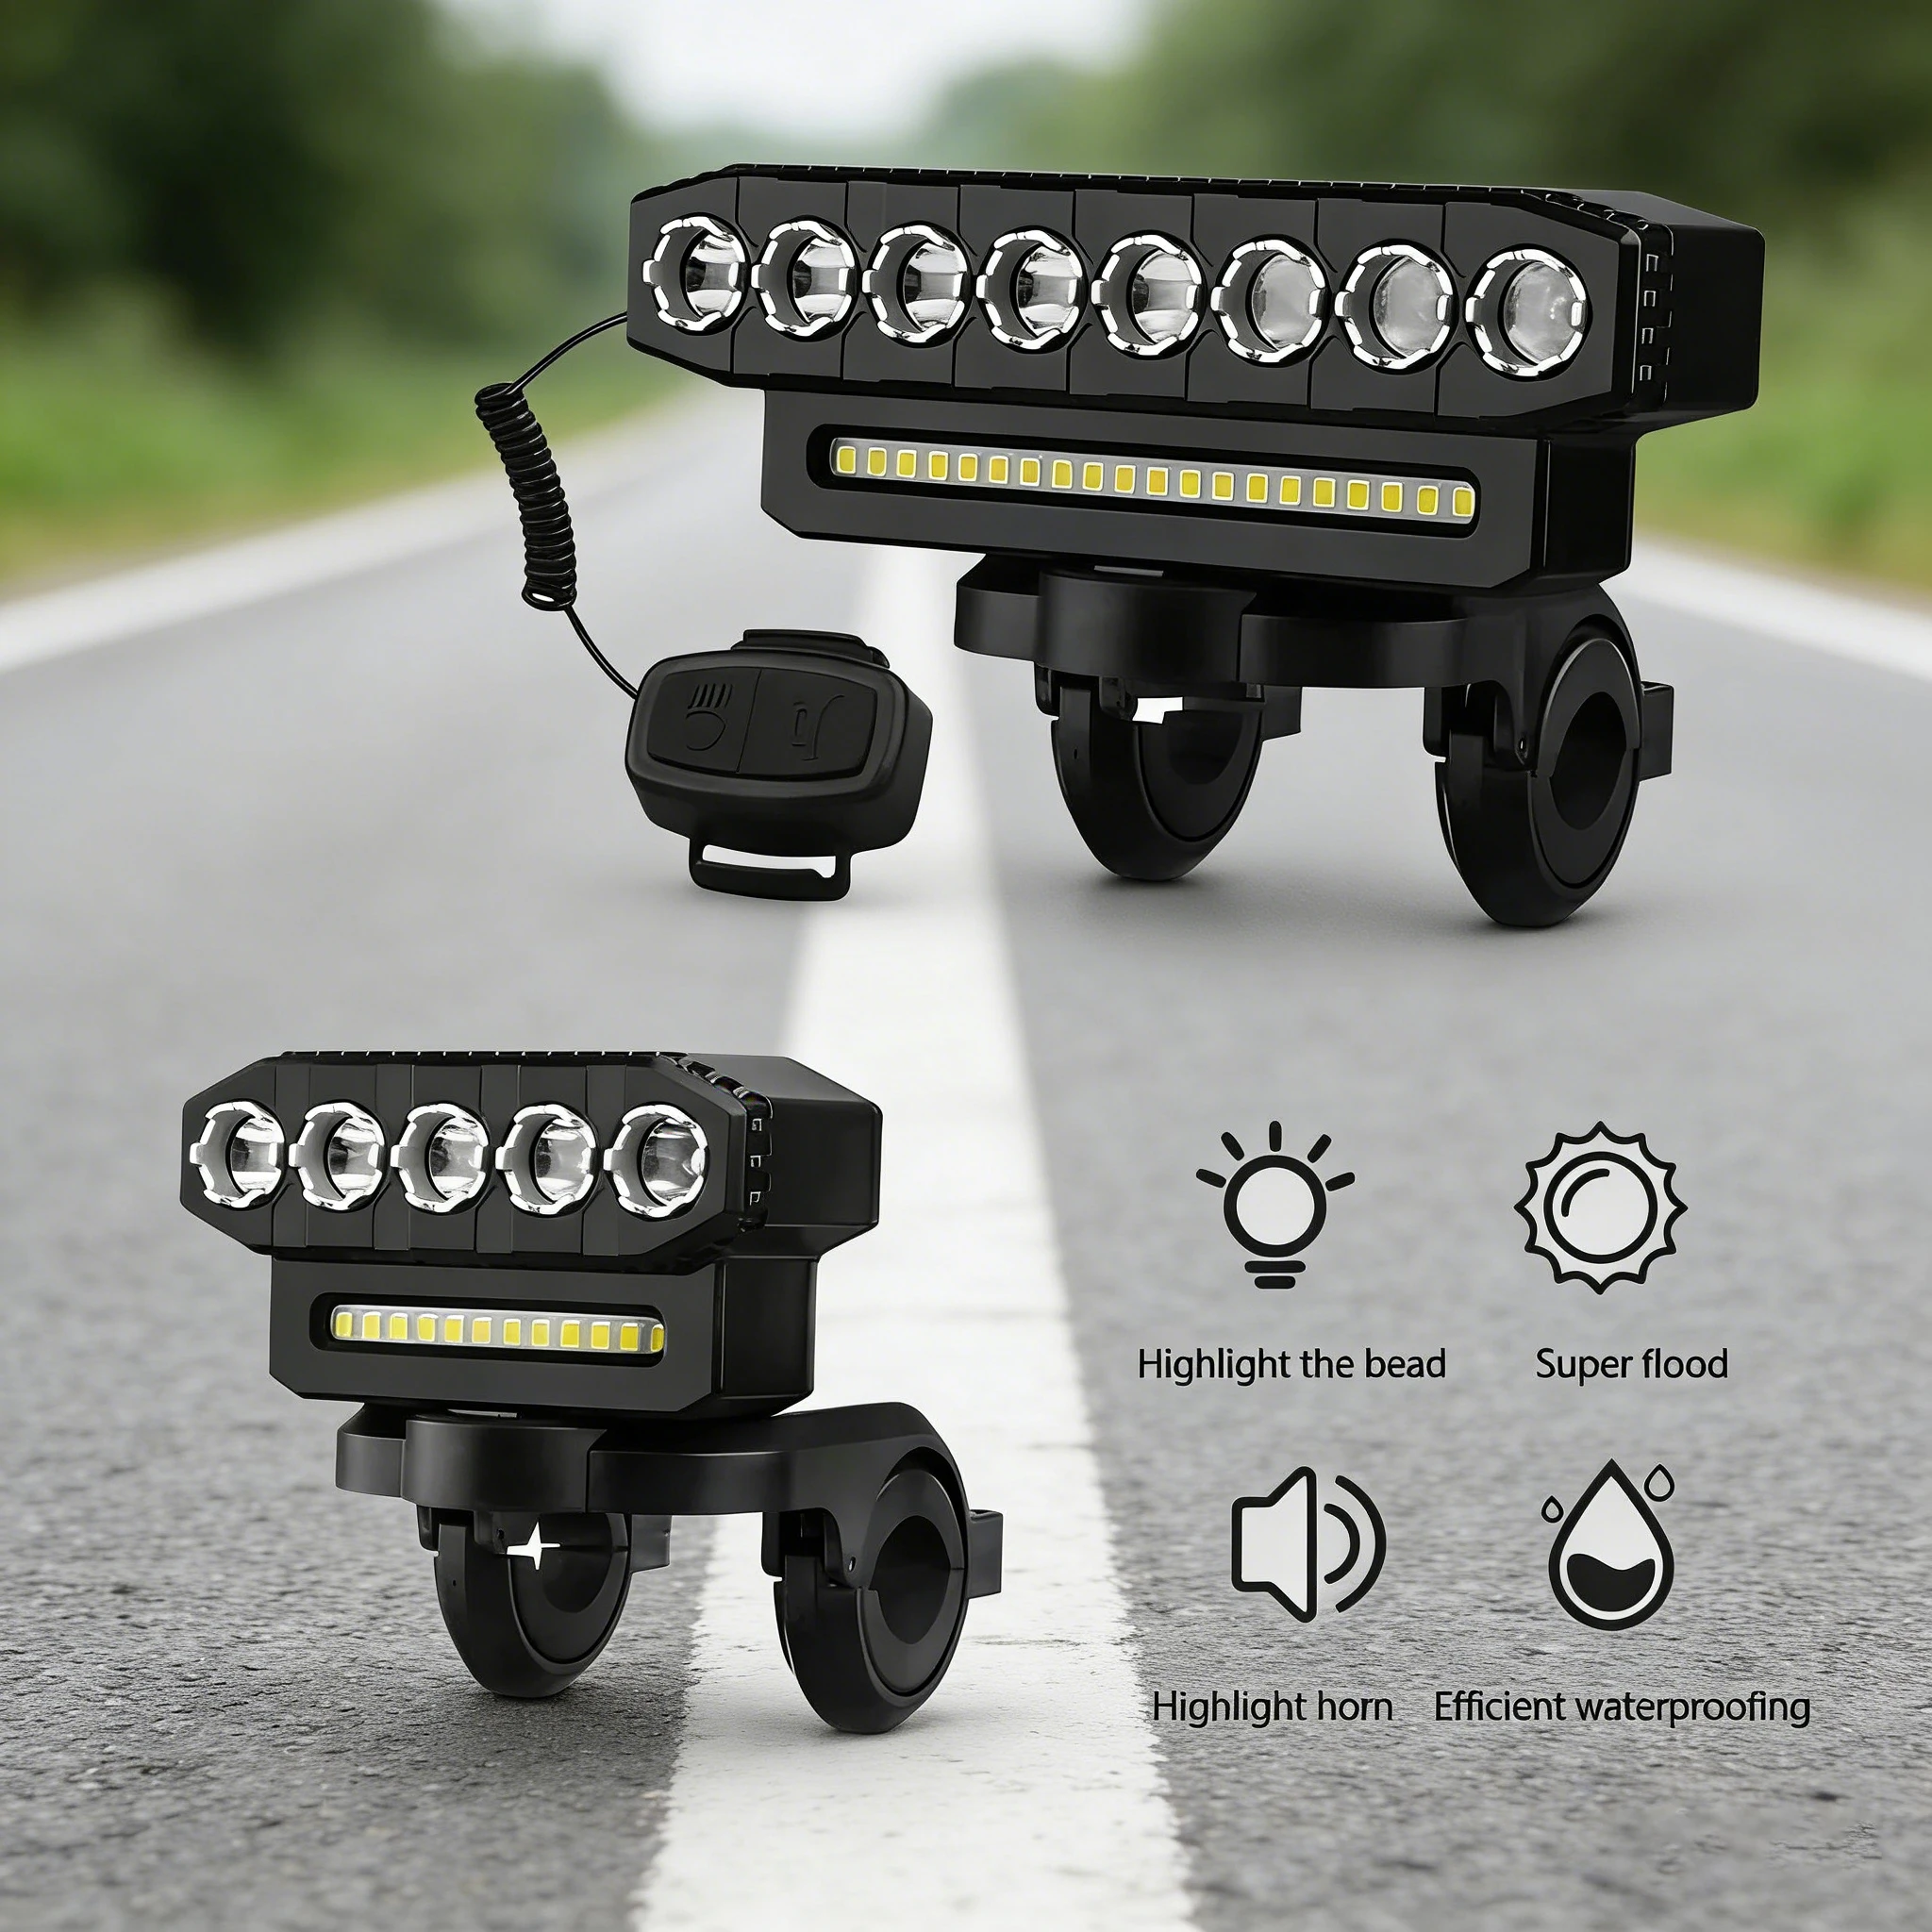
New USB Charging Bicycle Lights Night Riding High Bright Horn Lights
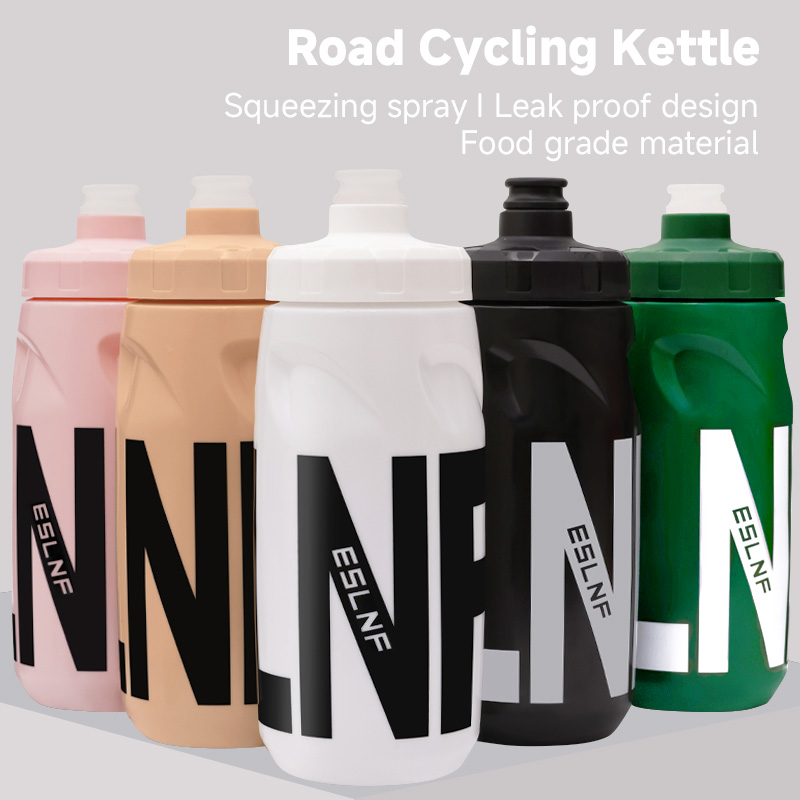
ESLNF 620ml Portable Squeeze Cycling Water Bottle Large Capacity
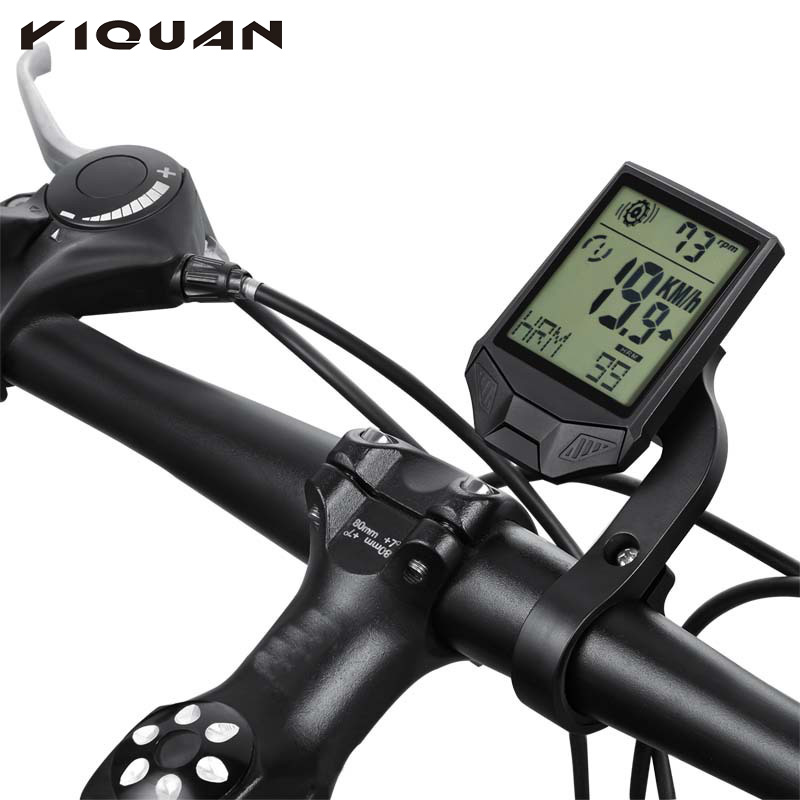
Wireless Waterproof Multi-Functions Cycling Computer Speedometer Odometer
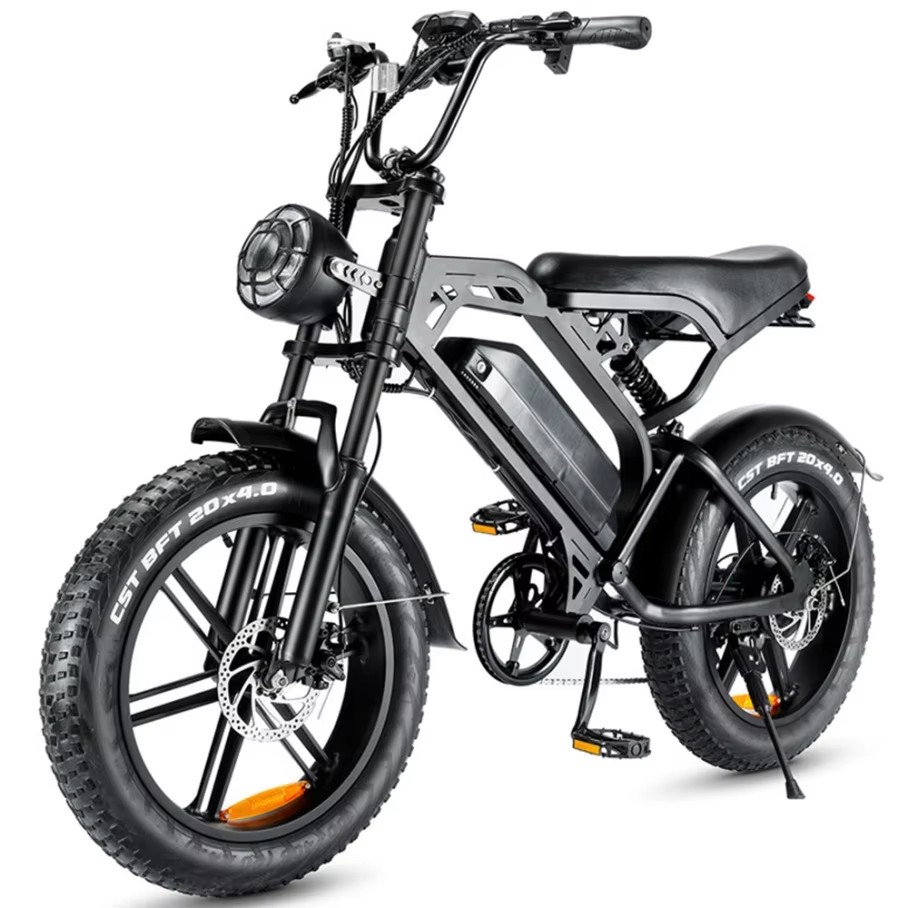
ESLNF EU V20 48V 250W-1000W Full Suspension Fat Tire Electric Bike
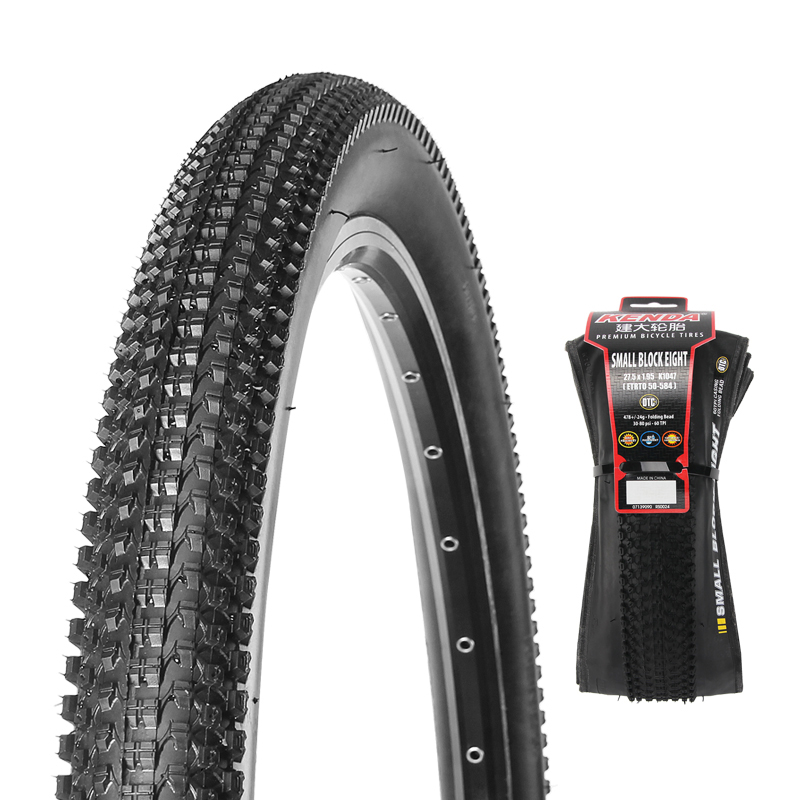
60TPI Casing Folding Beam Bike Fat Tire Wholesale High Quality Foldable
Engineering Precision in OEM/ODM CO2 Inflator Manufacturing
CO2 bike inflators represent an essential, safety-critical accessory where pneumatic physics, precision tolerance tooling, and thermal insulation intersect. Procuring at scale demands factory accountability, calibrated valve tolerances, and robust quality management systems.
Cryogenic Gas Dynamics & Joule-Thomson Mitigation
When compressed liquid carbon dioxide (under ~860 PSI / 59 bar pressure at 20°C) expands into a bicycle inner tube or tubeless tire casing, the Joule-Thomson effect rapidly cools the inflator head down to -40°C to -55°C. Substandard die-cast zinc alloys become brittle and suffer catastrophic micro-fractures under repeated thermal cycling. Our production lines use dedicated CNC turning centers machining aviation-grade 6061-T6 or 7075 aluminum alloy billets. We integrate custom EVA, polyurethane, and cold-resistant silicone sleeves to protect cyclists from frostbite injuries while preserving tensile integrity across thousands of discharge cycles.
Hermetic Micro-Valving & Dual-Valve Compatibility
A major quality failure point in cheap inflator designs is valve thread degradation and gas leakage during inflation. Our engineering team utilizes custom CNC internal thread-milling for threaded 3/8"-24 UNF cartridges (compatible with 12g, 16g, 20g, and 25g cartridges) paired with precision SUS304 stainless steel piercing needles. The internal flow path incorporates dual Presta and Schrader push-fit heads equipped with fuel-grade Viton (FKM) and HNBR O-rings, providing dependable sealing down to -45°C where conventional NBR rubber degrades and fails.
Flow-Regulation & Controlled Discharge Valves
Traditional non-regulated inflator heads puncture the canister and dump the entire gas volume instantaneously, blowing out ultralight TPU road tubes or freezing tubeless sealant into inactive latex balls. We engineer micro-metering twist-control valves and trigger-lock mechanisms that allow riders to pulse the gas flow. This enables controlled bead-seating on hookless tubeless rims followed by fine micro-inflation to exact operating pressures without wasting gas or damaging delicate tire casings.
OEM/ODM CO2 Inflator Head Architecture Comparison
Choose the right mechanical platform for your private-label target market. Every architecture is fully customizable with bespoke anodizing, laser-engraved logos, and blister or gift-box retail packaging.
| Architecture Type | Valve Control Mechanism | Material & Finishing | Sealing Compound | Target Category | OEM MOQ |
|---|---|---|---|---|---|
| Micro Push-On Valve | Spring-loaded direct push; gas flows upon pressing onto valve stem | CNC 6061 Aluminum, Hard Anodized (Type II) | Viton FKM / High-durometer Silicone | Ultra-compact road racing, weight-weenie saddle kits | 500 Units |
| Rotary Micro-Dial Flow Head | Precision internal needle valve operated via 90° or 180° dial | AL6061-T6 + Stainless 304 Needle, Multi-color Anodize | Dual HNBR Low-Temp O-Rings | All-road, Gravel bikepacking, Urban commuting | 1,000 Units |
| Ergonomic Trigger-Lock Inflator | Linear progressive trigger with integrated thumb safety slide | Reinforced High-Impact Nylon Body + Alloy Core | PTFE + FKM Cryo Seals | Enduro MTB, E-bike fleet emergency kits, Rental services | 1,000 Units |
| 2-in-1 Tubeless Plugs + CO2 Head | Integrated tubeless bacon strip insertion needle + dual inflator | Full CNC 7075 Aluminum, Knurled Grip Texture | Fluorosilicone extreme freeze rated | Competitive XC / Gravel & Enduro racing tiers | 500 Units |
Comprehensive Testing & Strict Quality Assurance Protocol
Every batch of OEM CO2 inflators undergoes 100% pneumatic pressure testing at 1,200 PSI to exceed cartridge operating thresholds. Samples undergo helium mass spectrometer leak detection ensuring a leakage rate under 1.0 × 10⁻⁵ mbar·l/s, salt spray corrosion testing exceeding ASTM B117 72-hour standards, and continuous thermal plunge cycles to guarantee zero mechanical jamming or catastrophic structural failure during emergency roadside situations.
Future Sourcing & Procurement Trends in Cycling Inflation (2025–2030)
B2B importers, bike brand product managers, and distributor purchasing leads must navigate evolving cyclist demands, shifting rim standards, and strict global environmental directives.
Tubeless & Gravel-Specific Sizing
The market share of tubeless setups across road, gravel, and mountain segments has exceeded 65% in premium markets. Standard 16g cartridges struggle to inflate 45mm gravel tires or 2.4" MTB tires up to pressure. Sourcing is shifting rapidly toward dual-threaded inflator heads compatible with 25g threaded cylinders and combined tubeless puncture repair forks, streamlining the cyclist's on-bike emergency repair kit.
TPU Inner Tube Protection
Thermoplastic polyurethane (TPU) inner tubes have overtaken butyl tubes among performance cyclists due to rolling resistance and weight advantages. However, TPU valve stems (especially plastic or unthreaded composite stems) are vulnerable to thermal distortion during instant CO2 discharge. Modern buyers require inflators engineered with variable throttling flow valves that prevent stem detachment.
Hybrid CO2 + Electric Micro-Pumps
While battery-powered micro electric pumps are rising in popularity, CO2 inflators remain unmatched in race conditions where seating a tubeless bead within 2 seconds is required. B2B procurement data shows brands bundling hybrid tool kits: a high-pressure CNC CO2 inflator head mounted directly onto a mini hand pump or pairing with rechargeable inflators for the ultimate peace of mind.
Plastic-Free Retail Packaging
Western European and North American retail channels demand 100% recyclable, plastic-free point-of-sale packaging. Our factory supports OEM clients with FSC-certified soy-ink printed unbleached kraft card wraps, molded sugarcane pulp trays, and hang-tag solutions compliant with EU Packaging and Packaging Waste Regulation (PPWR).
Factory Credentials, Machinery & Supply Chain Reliability
Kenus Intelligent Technology Co., Ltd. is strategically situated in Jinhua, Zhejiang—the core of China's premium cycling hardware, tooling, and export ecosystem.
TÜV Rheinland Verified Factory
Our workshop, assembly lines, trade reliability, and quality control systems are independently audited and certified onsite by TÜV Rheinland. We maintain transparent quality governance, comprehensive incoming raw material inspection (IQC), and documented traceability from alloy ingot to boxed carton.
Rapid 3D Prototyping & Tooling
With high-precision stereolithography (SLA) and metal 3D printing equipment in our R&D center, we turn industrial CAD designs into physical functional prototypes within 72 hours. Our engineering team assists brand managers in toolpath optimization, reducing overall unit mass while retaining critical pressure-bearing wall thickness.
International Compliance Portfolio
Our lighting, electronic, and pneumatic accessories comply with global market regulations. We hold documented CE certificates (SIT230614230201E), RoHS chemical compliance (SIT240417230101R), Japanese PSE certifications (SIT240226230301P), and EMC inspection reports (SIT250212230201ER), ensuring seamless customs clearance.
Frequently Asked Questions: OEM/ODM CO2 Inflator Sourcing
Key technical, commercial, and regulatory questions addressed by our engineering and logistics specialists.
What is the minimum order quantity (MOQ) for custom private-label inflators?
Standard OEM orders with laser-engraved logos and custom-anodized colors start at 500 to 1,000 units depending on the valve model. Ready-to-ship neutral stock for sampling and qualification runs can be dispatched from 2 to 50 pieces.
Can you supply both threaded and non-threaded cartridge designs?
Yes. Our primary product line focuses on precision CNC 3/8"-24 UNF threaded heads, which represent 90%+ of Western consumer demand. We also engineer fully enclosed canister holders with puncture pins that accommodate unthreaded 16g cartridges.
How do you prevent gas freezing injuries during use?
We supply custom high-density EVA, neoprene, or silicone insulating sleeves branded with your logo. In addition, we manufacture full-body enclosed alloy inflator capsules where the cartridge sits inside an insulated canister, eliminating direct skin contact with freezing metal.
Are the inflator heads dual-compatible with Presta and Schrader valves?
Yes. Our valve chucks feature auto-switching or reversible internal grommets. Cyclists can press or thread directly onto either a road Presta or MTB Schrader valve without needing cumbersome brass adapters or manual internal rebuilds.
Do you manufacture or ship CO2 gas cartridges directly?
We manufacture the CNC inflator hardware, freeze jackets, mounting brackets, and tubeless repair forks. For clients requiring turnkey cartridges, we partner with certified gas filling plants. Filled cartridges fall under UN 2037 / Class 2.2 dangerous goods regulations for maritime freight.
What surface treatments and colorways can you achieve?
We offer Type II sulfuric acid anodizing in high-luster and matte finishes (Black, Gunmetal, Anodized Blue, Orange, Red, Olive Green, Purple, and Raw Polished). We also provide laser ablation, screen printing, and CNC machined chamfer details.
What is the lead time from CAD sign-off to bulk shipment?
Rapid 3D prototypes are delivered within 3-5 days. CNC pre-production sample sign-offs take 15 days. Mass production lead times generally range between 25 and 35 calendar days depending on order volume and packaging specifications.
How do you ensure zero leakage across wide temperature fluctuations?
Our internal seal package utilizes hydrogenated nitrile butadiene rubber (HNBR) and genuine Viton elastomers rated from -45°C to +150°C. Each production lot is subjected to liquid nitrogen thermal immersion tests followed by 12-hour pressure retention audits.
Ready to Develop Your Private-Label CO2 Inflator Line?
Connect with our technical sales engineers in Zhejiang. Submit your specifications, target quantities, and custom packaging requirements to receive a fast engineering review and formal quotation within 24 hours.